Two names come up in almost every steel formwork quotation: St 37 and St 52. These are the old DIN designations; their current European equivalents are S235JR and S355J2. A mould is not built from a single grade; which part uses which is decided by calculation.
The basic difference
| St 37 (S235) | St 52 (S355) | |
|---|---|---|
| Yield strength | ~235 N/mm² | ~355 N/mm² |
| Tensile strength | 360–510 N/mm² | 470–630 N/mm² |
| Strength difference | — | About 50% higher |
| Modulus of elasticity | 210,000 N/mm² | 210,000 N/mm² (identical) |
| Weldability | Very good | Good, may need preheating |
| Cost | Lower | Higher |
| Availability | Easy in all sections | Lead time in some sections |
The critical point: the modulus of elasticity is the same for both. St 52 is stronger, but in the same section it does not deflect less. Because panel flatness is a deflection question, you cannot solve a surface quality problem by raising the steel grade — you have to increase the section or tighten stiffener spacing.
Where each is used
St 37 (S235) — most of the mould
- Panel plate
- Stiffening profiles
- Working platform, handrail, ladder
- General structural members
St 52 (S355) — where load concentrates
- Lifting lugs and anchor plates
- Main trusses carrying high loads
- Shafts, pins and hinge connection zones
- Tie plates and jack seats
- Confined areas where the section cannot be enlarged
The logic: St 52 where weight and space are constrained, St 37 everywhere else. Building the whole mould in St 52 raises cost without improving deflection, so it rarely pays.
The welding side
St 52 has a higher carbon equivalent. In practice this means:
- Preheating may be required in thick sections and cold conditions
- Rapid cooling after welding carries a cracking risk
- Where grades are mixed, the electrode is selected for the lower-strength material
- Weld sequence and direction govern distortion from shrinkage — panel flatness is won or lost here
Weld shrinkage is a real problem in panel fabrication: runs are distributed symmetrically and panels are straightened after welding.
Cold climates and impact toughness
The letters at the end of the designation state the temperature at which impact toughness is verified:
- JR — +20 °C
- J0 — 0 °C
- J2 — −20 °C
For parts used in winter conditions, subject to impact, or lifted by crane, J2 is preferred. On a lifting lug this is not a detail — it is a safety matter.
The cost balance
St 52 costs more per tonne than St 37. In return, its higher strength means less material in some parts. The right comparison is not the price per kilogram but the total cost per part — and the deflection limit enters the decision too.
How we work
On every project we proceed as follows:
- Fresh concrete pressure and vertical loads are calculated
- Panel plate and stiffening are dimensioned to the deflection limit (1 mm over 2 m for exposed concrete, 2 mm otherwise)
- Main structural sections are selected for strength
- Connections where load concentrates, and lifting components, are raised to St 52
- Weld details and sequence are planned to minimise distortion
That is why our quotations say "steel grade: St 37 or St 52 — per project requirement": the grade is not a marketing label, it is the output of a calculation.
In short
St 52 is stronger but no stiffer in the same section. The right approach in formwork is to build the body in St 37, raise load-concentrated points to St 52, and solve panel flatness with section size and stiffener spacing.
PRODUCT GROUPS IN THIS ARTICLE
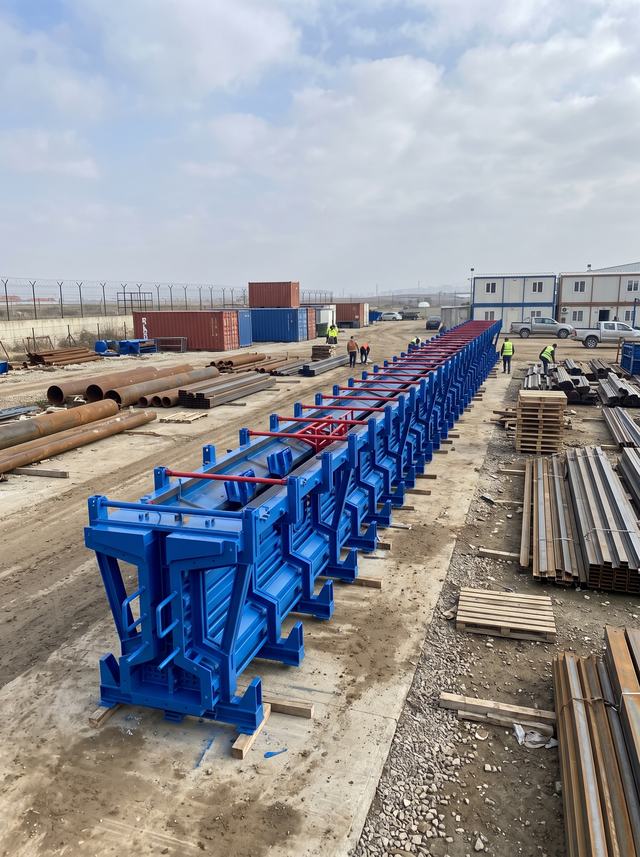
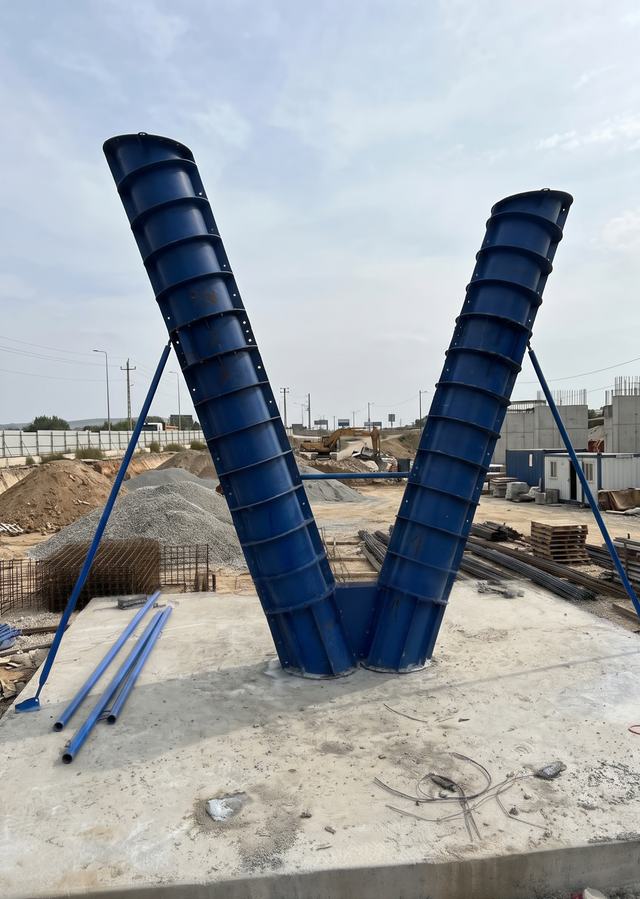
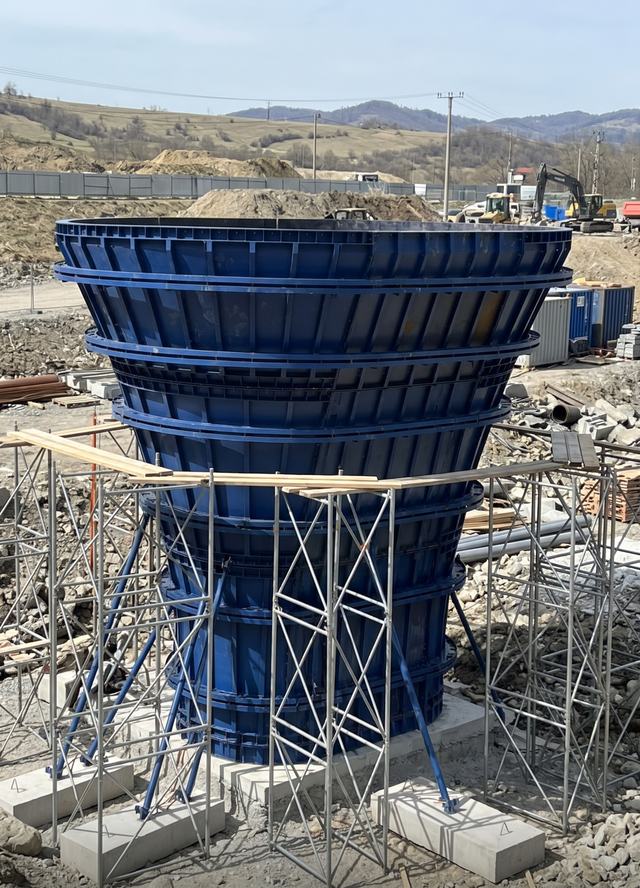
Let us work out the right formwork configuration for your project.
REQUEST A QUOTE